Long-term protection depends on matching the coating system to the service environment, then controlling every stage from steel preparation to repair. By the end, you will be able to compare galvanizing, epoxy, polyolefin, polyurethane and paint systems, define plant controls, and judge whether inspection records support the expected service life.
Key takeaways
- Match the coating to temperature, immersion, soil, UV, abrasion and service-life demands.
- Remove mill scale, rust, oil and moisture before coating the steel.
- Control steel temperature, application rate, cure time and line speed together.
- Record thickness, holiday tests, repairs, standards and batch details for traceability.
Which coating system fits the tube’s service environment?
Match the coating to the service, not simply the tube’s appearance or nominal thickness. Start with operating temperature, immersion or burial, soil chemistry, ultraviolet exposure, abrasion, tube dimensions and required service life.
| System | Best fit | Main caution |
|---|---|---|
| Hot-dip galvanizing | Atmospheric exposure and selected immersion or buried service; zinc provides sacrificial protection. | Check soil and water chemistry, steel grade, wall thickness, tolerances and temperature. |
| Three-layer polyethylene | Buried pipelines needing moisture, corrosion and impact protection. | Confirm temperature rating and interface qualification. |
| Three-layer polypropylene | Buried lines requiring higher temperature capability than polyethylene. | Verify impact, cathodic-disbondment and thermal-ageing results. |
| Fusion-bonded epoxy (FBE) | Buried or immersed steel where adhesion and corrosion resistance lead. | Add mechanical protection for severe handling or abrasion. |
| Liquid epoxy | Field repairs, complex geometry and selected immersion service. | Control mixing, humidity, temperature and cure time. |
| Polyurethane | Above-ground lines needing UV and abrasion resistance over a compatible primer. | Specify the complete coating system, not polyurethane alone. |
| Powder coating | Factory-controlled above-ground tubes and repeatable protective finishes. | Do not assume suitability for burial, immersion or high temperature. |
| Paint | Atmospheric maintenance or lower-demand protection. | Plan more inspection and recoating than with a qualified multilayer system. |
For potable-water service, select a system with approval for that contact, not a general industrial grade. A three-layer system can look sound outside while its FBE barrier or adhesive interface has failed, so qualify and inspect each layer.
Qualify repair materials against the original coating and service temperature. Matching colour or thickness does not prove compatible water-vapour resistance, curing or cathodic-disbondment performance.
What must happen before the coating reaches the steel?
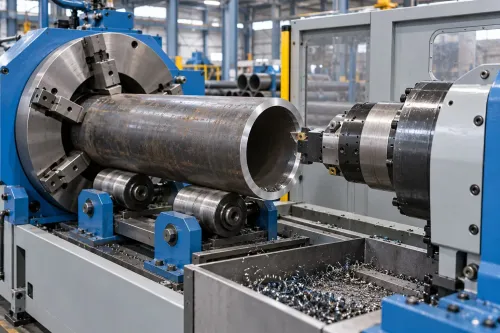
Oil, mill scale, soluble salts and weld contamination must be removed before coating begins. A thick coating cannot compensate for a weak interface; it will blister, delaminate or lift from the steel.
Use the preparation route that matches the tube and coating specification:
- Remove oil and grease by degreasing before blasting or chemical treatment. Residue can spread across the surface and contaminate abrasive.
- Remove scale and rust by abrasive blast cleaning to ISO 8501-1 Sa 2½, or by pickling where the process specification permits it. Pickled steel needs thorough rinsing, neutralisation and drying.
- Grind weld spatter, sharp projections and adherent weld slag. These defects create thin spots and stress points in the finished film.
- Specify the surface profile by measured amplitude and required angularity, not by Sa 2½ alone. The profile must suit the coating thickness and chemistry.
- Remove blast dust and verify soluble-salt levels before coating. Flash rust, embedded abrasive and reused abrasive contaminated with oil or salts can defeat an otherwise clean-looking surface.
| Contamination | Required control | What goes wrong if missed |
|---|---|---|
| Oil or grease | Alkaline degreasing before blasting | Poor wetting and widespread delamination |
| Mill scale or rust | Sa 2½ abrasive blast cleaning or controlled pickling | Rust returns beneath the coating |
| Weld slag or spatter | Grinding and visual inspection | Voids, pinholes and edge lifting |
| Dust or soluble salts | Vacuum removal, clean rinse and salt testing | Osmotic blistering and underfilm corrosion |
Release the tube only when it is clean, dry, correctly profiled and free from visible flash rust. Keep abrasive recovery systems separated, filtered and replaced against defined contamination limits; indefinite recirculation can put the failure back onto every tube.
How does the plant control heating, application and curing?
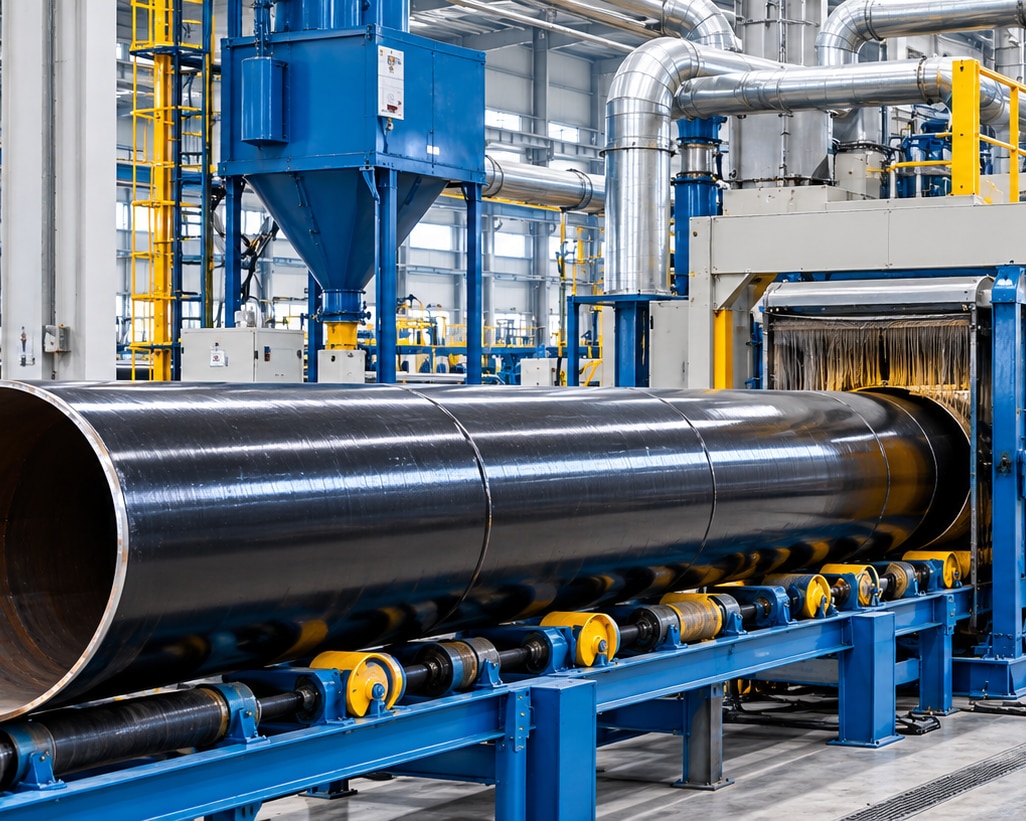
An acceptable average temperature can hide a cold weld seam, tube end or shaded section. Control the thermal history at the coating location, not only the oven display.
- Preheat with induction preheating or another controllable source, then measure steel temperature around the circumference and at vulnerable features. Keep steel at least 3 °C above dew point; log both values because cooling during a line stop can cause condensation.
- Apply powder or liquid only within its specified application range. For fusion-bonded epoxy, match steel temperature to the powder’s gel and cure window; excessive heat can damage the coating while cold areas remain under-cured.
- For polyethylene or polypropylene, control adhesive and polymer extrusion temperature, die pressure, layer thickness and contact with the heated steel. A stable melt does not compensate for insufficient steel heat or contaminated contact surfaces.
- Hold the required cure dwell before cooling. Confirm that the slowest zone, including welds and ends, receives enough time and heat; raising oven temperature alone can overheat the surface while leaving geometric cold spots.
- Cool in a controlled manner before handling, inspection or repair. Quenching too early can distort layers or lock in weak intercoat bonding.
- Set line speed from the slowest validated step: cleaning, heating, application, cure, cooling or inspection. Increasing speed without re-establishing the required thermal history is a direct route to under-cure and poor adhesion.
Record tube identity, line speed, steel temperature, coating batch, settings and any stop or repair so failures can be traced to a process excursion.
How do you verify coating thickness, holidays and vulnerable tube features?
A single DFT reading cannot prove uniform protection. Calibrate magnetic and eddy-current gauges on a representative coated sample, then use the measurement areas, frequency, acceptance rules and calibration checks defined by ISO 19840.
Sample the weld seam, both ends, edges, overlaps, supports and the underside as the tube rotates; inspect the thinnest reading, not the convenient one.
| Feature | Confirm | Typical failure or response |
|---|---|---|
| Longitudinal or circumferential weld | DFT, adhesion and holiday detection under ASTM G62 | Treat weld spatter, shadowing or low build before release |
| Ends, bevels and threads | Full visual access, DFT and continuity | Keep the specified cutback clear; repair exposed steel without filling functional threads |
| Edges and dents | Edge coverage, impact damage and DFT | Feather sharp runs; reject coating cracked over a dent until assessed |
| Handling marks and supports | Visual inspection, DFT and holiday scan | Remove loose coating, abrade sound edges and recoat |
For each holiday, record tube identification, location, size, cause and repair material. Remove loose or contaminated coating, feather the perimeter, clean the steel, apply the approved compatible material at its specified recoat thickness and cure it fully.
Recheck DFT and repeat the ASTM G62 scan; a patch that passes thickness but still leaks is not acceptable.
When reviewing equipment from Gallium Equipment Pvt. Ltd., require controlled tube rotation and gun access so weld undersides, ends and support contact zones are inspectable rather than hidden production blind spots. Keep qualification tests—adhesion, impact and thermal ageing—separate from routine release checks.
Which standards and records make long-term performance defensible?
A defensible file links the coating, the steel, the test result and the service conditions. A thickness reading alone cannot prove durability: soluble salts, poor adhesion, flash rust or uncured material can cause failure beneath a thick film.
| Standard | What it establishes | Evidence to retain |
|---|---|---|
| ISO 1461 | Hot-dip galvanized coating requirements for fabricated steel articles | Bath records, coating thickness results, visual inspection and repair log |
| ASTM A123 | Zinc coating requirements for iron and steel products | Lot identification, mass or thickness measurements, inspection results and certificates |
| ASTM A53 | Steel pipe requirements, including provisions for galvanized pipe | Pipe grade, dimensions, heat number and conformity documents |
| ISO 21809 | External coating systems for buried or submerged pipeline components | System qualification, application parameters, inspection and repair records |
| ISO 12944 | Selection and qualification of protective paint systems by corrosivity category | Environment classification, paint data sheets, DFT and cure records |
Qualification testing should cover adhesion, cathodic-disbondment resistance, impact or indentation, peel or shear performance and thermal ageing for the specified system. Record the substrate preparation, profile, coating batch, test temperature and failure mode, not just “passed”.
Routine production records should capture heat or tube number, blast profile, dust and salt results, steel temperature, line speed, application settings, cure, dry-film thickness, holiday results and inspector identity. Use ISO 8502-6 extraction and ISO 8502-9 conductivity measurement with the purchaser’s acceptance limit.
Qualify repair materials and procedures against the original system and service temperature. A colour match or equal thickness does not prove compatible barrier performance or cathodic-disbondment resistance.
Frequently asked questions
How do you choose a tube coating system for its service environment?
Assess operating temperature, immersion or burial, soil chemistry, ultraviolet exposure, abrasion, tube dimensions and required service life before selecting the coating.
What preparation must occur before coating reaches the steel?
Clean the tube by removing oil, grease, mill scale, rust, dust and moisture, then confirm the prepared surface meets the specified cleanliness and profile.
How does a coating plant control heating, application and curing?
Coordinate steel temperature, coating application rate, line speed, film formation and cure conditions, while recording process values against the coating specification.
How do you verify coating thickness, holidays and vulnerable tube features?
Measure dry-film thickness, test for pinholes or holidays, inspect welds, ends, seams and handling damage, and repair defects before release.
Which standards and records support defensible coating performance?
Keep the coating specification, inspection plan, test methods, equipment calibration records, batch numbers, process logs, repair records and final acceptance results.