A strip-processing line can keep forming, slitting or finishing steel while the entry section changes coils only when the accumulator contains enough usable reserve. By the end, you will be able to calculate that reserve, distinguish charging from discharging, compare horizontal and vertical layouts, and define the controls needed to move a splice through the line safely.
Key takeaways
- Calculate reserve from line speed, coil-change time and usable carriage stroke.
- Use loop sensors and tension control to prevent strip slack, skew and overrun.
- Sequence the splice so the downstream mill crosses it without stopping.
- Specify strip width, thickness, grade, speed and joining method before integration.
How the accumulator bridges a coil change
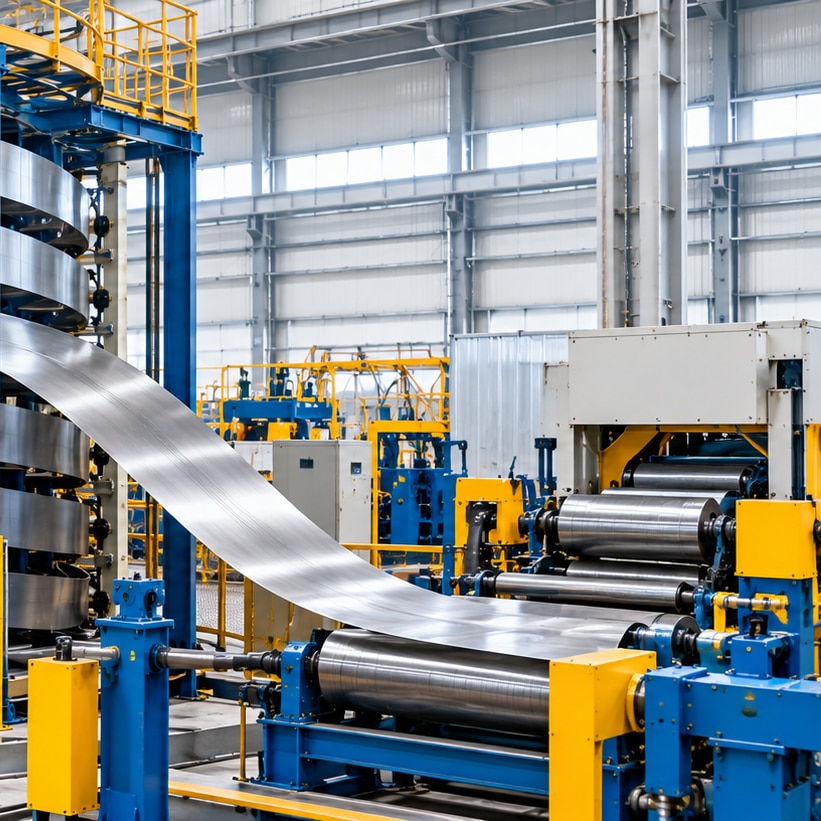
A coil accumulator system stores strip as loops between fixed rolls and a movable carriage, creating a finite strip buffer between the entry equipment and the continuously running mill. As the carriage moves, it increases or reduces the loop length without interrupting the downstream forming, welding or finishing process.
The operating sequence has three phases:
- Charging cycle: Before the old coil reaches its end, the entry section feeds strip faster than the downstream line consumes it. The carriage travels to create the required loops, while sensors regulate strip tension and confirm that usable reserve is available.
- Storage cycle: The carriage holds those loops at a controlled position while the line runs at production speed. Payoff speed matches line demand, preventing slack, excessive tension or a loop collapse.
- Discharging cycle: When the entry section stops to cut, remove and replace the coil, the downstream line draws strip from the accumulator. The carriage moves back, releasing stored length at the line’s required speed.
During this discharge, the operator positions the new coil, trims both ends and makes the butt weld. The accumulator keeps production moving until the joined strip reaches the line. The splice still needs stable guidance, bead removal or inspection where specified; reserve length cannot rescue a weld that snags or fails.
Once the splice passes, entry speed rises to refill the buffer and restore the storage position. When the reserve runs out, the downstream line stops.
How much strip reserve does the line need?
Calculate the minimum usable strip length as:
usable strip length = line speed × bridging time
For metres per minute and seconds, use: line speed × time ÷ 60. A 100 m/min line facing a 60-second interruption therefore needs 100 m of usable reserve before any margin is added.
Define the interruption precisely. Add the coil-change time, welding time, operator actions and any threading or splice-inspection delay. If the stated coil-change time already includes welding, do not count the welding cycle twice.
Use this accumulator capacity calculation checklist:
- Set the operating line speed, not the machine’s advertised maximum.
- Convert the full interruption into seconds and multiply by line speed.
- Add time for acceleration back to production speed and the strip length consumed during deceleration or stopping.
- Add a control margin for weld-cycle variation, operator response and recovery from a misaligned splice.
- Subtract the reserve that must remain to prevent the final loop from collapsing.
For example, a 100 m/min line with 45 seconds for coil changing and 8 seconds for welding needs 88.3 m before margins: 100 × 53 ÷ 60. With an additional 15% allowance, specify at least 101.5 m of usable reserve.
Do not confuse gross geometric capacity with production capacity. End-of-travel zones, loop-stability limits, splice passage and minimum operating reserve make the usable length smaller than the total strip held by the rolls. A capacity quoted only in seconds is incomplete unless it states the reference line speed and minimum reserve.
Choosing the layout and controlling the strip
Choose a horizontal accumulator when easy threading, cleaning and inspection matter more than floor space. Its low working height simplifies strip handling and keeps operators away from elevated moving loops, while its longer footprint needs more plant area.
A vertical accumulator suits a compact floor plan, provided the building has sufficient height and safe access to upper rolls.
| Layout | Main advantage | Main trade-off |
|---|---|---|
| Horizontal accumulator | Low line height, accessible rolls and straightforward strip handling | Larger floor footprint |
| Vertical accumulator | Smaller floor footprint and compact lengthwise arrangement | Greater height, more demanding access and guarding |
Keep stored strip stable with guided rolls, adequate roll diameter and aligned entry and exit paths. Check roll diameter, wrap angle and the number of reversals against strip grade, thickness, yield strength and surface finish; repeated tight bending can mark high-strength or surface-critical strip.
Use dancer rolls to absorb speed changes and maintain controlled tension, not a fixed mechanical pull. Pinch rolls at suitable entry or exit points prevent backslip and help isolate the stored loop from downstream speed changes. Loop control should use position sensors with plausibility checks, upper and lower limits, and coordinated payoff and line-speed commands.
Specify guarded access, emergency-stop behaviour and cleaning access around rolls and guides. Dirty or slipping rolls, wandering strip, failed sensors and overfilled loops can destabilise the reserve; underfilled loops can stop the line before the splice arrives. Define how the system isolates a break and safely rethreads the strip.
Managing the coil-change sequence and splice passage
The last metres of the old coil trigger a controlled handover, not an immediate stop. The control system raises the accumulator reserve beforehand, matches the downstream line speed, and coordinates strip tension, loop position and decoiler speed while the operator prepares the entry equipment.
1. Confirm the reserve is above the calculated changeover limit. Check strip tracking, sensor signals and tension before the old coil reaches its end; an underfilled accumulator leaves no time to correct a delayed coil change.
2. Slow and stop the decoiler when the tail reaches the cut position. The shear welder removes the old tail, while the coil car withdraws the empty coil and brings the prepared coil into alignment.
3. Keep the downstream mill running from stored strip. The operator threads the new head, clamps it in the shear welder and completes the butt weld before the accumulator reaches its minimum reserve.
4. Release the joined strip into the line at controlled speed. During splice passage, guides, rolls and tooling must accept the thicker or uneven weld area without catching it; a seam detector or marked splice zone can direct the joint to a reject station.
5. Record the weld inspection result before restoring normal entry speed. If the weld fails inspection, isolate or reject the splice while reserve remains; if it passes, trim or remove the bead where specified, re-establish tension and refill the accumulator.
A failed weld, wandering strip or false position signal can exhaust the reserve and stop production. Define the alarm, safe stop and recovery sequence before commissioning.
What to specify before integrating an accumulator
A line-speed rating alone does not select an accumulator. Record the process, maximum and minimum speed, coil-change interruption, splice dimensions, stopping distance and required usable reserve, then define how charging, discharging and refill signals will coordinate with the payoff and downstream drive.
Before requesting a layout, specify:
- Material width, thickness, yield strength, grade, surface finish and edge condition; these determine roll loading, bending force, minimum roll diameter, loop stability and marking risk.
- Strip tension control limits, allowable tension changes, threading direction and the position of the tension dancer or load cell.
- Splice weld thickness, bead removal, seam detection, weld-strength check and the method for rejecting a defective joint.
- Guarding, emergency-stop behaviour, access for roll cleaning and inspection, sensor plausibility checks, and protection against strip wandering or loop overfill.
- Fault recovery after a strip break, including where operators isolate stored energy, cut the strip, rethread it and reset the accumulator without releasing an uncontrolled loop.
| Process | Verify before connection | Main risk |
|---|---|---|
| Forming mill | Splice clearance through guides, rolls and tooling; restart speed and tension limits | A raised weld catches tooling or damages the profile |
| Slitting line | Knife width, slit-edge quality, lane stability and splice detection | A wandering or burred edge destabilises loops |
| Cut-to-length line | Cut synchronisation, splice rejection and restart reference | A splice produces an off-length or rejected blank |
Give these details to the integrator; Gallium Equipment Pvt. Ltd. can use them to match the accumulator’s mechanical envelope and controls to the actual line rather than its headline speed.
Related product
 | COIL ACCUMULATOR SYSTEMS Gallium Horizontal Accumulators are available in several models based on Strip width range, Coil thickness and Operating line speed options. View product → |
Frequently asked questions
How does a coil accumulator bridge a coil change?
It stores strip in loops while the entry section changes coils, allowing the downstream mill to continue running from the stored reserve.
How much strip reserve does the line need?
Set reserve from downstream line speed multiplied by the time needed for coil removal, new-coil loading, threading, joining and acceleration, then verify it against usable accumulator stroke.
How do you choose an accumulator layout and control the strip?
Compare horizontal and vertical layouts against available space, strip path, access and capacity, then use loop-position sensing, tension control and edge guidance to keep the strip stable.
What should you specify before integrating an accumulator?
Provide strip width, thickness, material grade, line speed, coil dimensions, changeover time, joining method, splice limits, tension range, available footprint and control-system interfaces.